
 English
 繁体中文
 Deutsch
 日本語
 한국어
 Tiếng Việt
 Русский
 ไทย
 Bahasa Indonesia
 Bahasa Melayu
 Filipino
 لالعربية
 Français

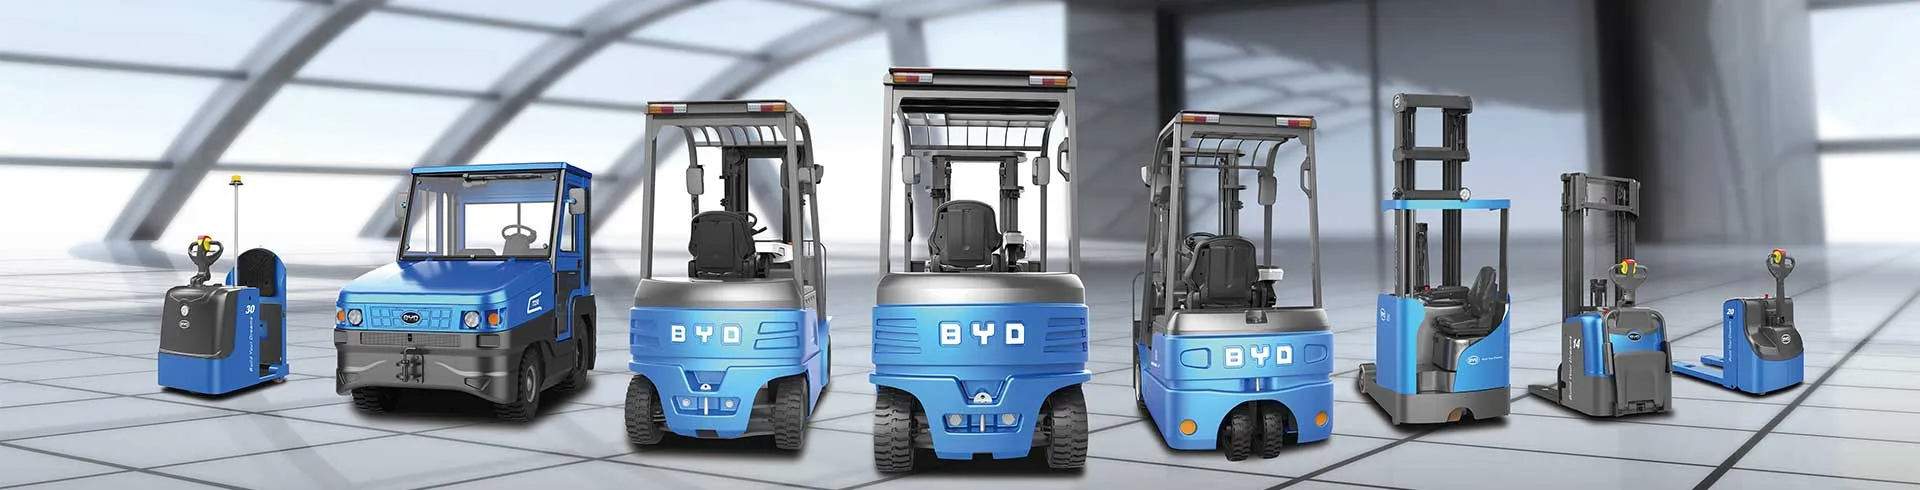
Pharmaceutical production and logistics scenarios have strict zoning requirements for ambient temperature areas and low-temperature cold storage zones, as different pharmaceutical products including oral solids, injections, biological agents and vaccines have distinct storage temperature rules that must be strictly followed to avoid quality risks. Many operation teams used to arrange the same forklift to travel between two different temperature zones, which will easily cause hidden dangers such as condensation on mechanical and electrical components, cross-temperature residue that may contaminate pharmaceutical materials, and even damage the temperature stability of sensitive products. It is a widely recognized standard-compliant practice now to deploy separate dedicated forklifts for cold zones and ambient pharma zones respectively, which can effectively reduce cross-contamination risks, extend the service life of handling equipment, and help enterprises meet the GMP inspection requirements for pharmaceutical production and storage. The forklift for ambient pharmaceutical zones is designed with clean, non-shedding material for all outer surfaces, no dead corners for easy cleaning and disinfection, with low noise operation that will not disturb the stable production environment. The cold zone dedicated forklift is equipped with special low-temperature resistant battery, anti-freeze lubricant and sealed waterproof electrical structure, which can run stably for long hours even under continuous low temperature working conditions. Jianshu New Energy provides tailored overall electric forklift deployment plans for pharmaceutical industry clients, and we can also offer proper model matching reference with BYD Forklift product lines to meet different site size, load weight and working hour demands. If you have any demand for pharmaceutical industry dedicated material handling solutions, you can send your detailed requirements to 17399989919@163.com for further professional consultation. Implementing separate forklift management for different temperature zones does not require excessive extra investment, but can bring long term returns on equipment maintenance cost reduction, pharmaceutical product quality risk avoidance and audit pass rate improvement, which is a highly cost-effective optimization measure for all pharmaceutical production and logistics enterprises.


